Magnetic stainless steel includes ferritic, martensitic and duplex grades. Austenitic grades such as 301, 304 and 316 generally show little magnetic attraction when properly solution annealed, but processing can change their response. For purchasing, distinguish alloy identification from magnetic performance: specify the required material condition, an appropriate test method and an acceptance limit rather than relying on whether a handheld magnet sticks.
A magnet test can raise a useful question about stainless steel, but it cannot answer every question about the material. A buyer may want to verify a coil’s grade, an engineer may need a component that minimally disturbs a magnetic field, and a designer may deliberately want strong magnetic attraction. Those are different requirements.
For Myriad foil and precision-strip enquiries, the practical starting point is to identify which requirement matters to the finished part. A description such as “non-magnetic stainless steel” leaves important details unresolved: does it apply to incoming strip, a bent component, a weld, or the complete assembly?
This guide explains the material families, why 301, 304 and 316 can respond differently after fabrication, and how to turn a magnetic requirement into a specification that a supplier and testing laboratory can evaluate.
Ferritic, martensitic and duplex stainless steels are ferromagnetic. Austenitic stainless steels generally have low magnetic permeability when their structure remains austenitic. The distinction depends on microstructure, rather than the presence of the word “stainless” in a material description. Outokumpu identifies these differences in its stainless steel types guide.
Material family | Representative grades | General magnetic behaviour |
Ferritic | 430 | Magnetic; attraction is normal for this family |
Martensitic | 410, 420 | Magnetic; processing and heat treatment affect properties |
Duplex | 2205 | Magnetic because the structure contains ferrite |
Austenitic | 301, 304, 316 | Usually low magnetic response when solution annealed; processing can change it |
This table is a family-level guide, not a list of guaranteed permeability values or supplier stock. It should help narrow an investigation, not replace a purchase specification.
Many familiar steels, including ordinary carbon steel, are magnetic at room temperature. However, “steel” describes a broad class of alloys, so it does not establish one universal magnetic response. ASSDA’s grade-confirmation guide distinguishes magnetic carbon and stainless steels from annealed austenitic grades.
No. A magnetic stainless steel can be the correct material for its intended service. Corrosion resistance comes from alloy chemistry and the protective surface film, and suitability depends on the environment. Magnetic attraction alone is not a corrosion test or a quality ranking. See Outokumpu’s explanation of stainless steel properties.
For procurement, ask what the magnet observation actually changes. If the drawing contains no magnetic requirement, investigate grade identity and other acceptance criteria separately before rejecting material solely because it attracts a magnet.
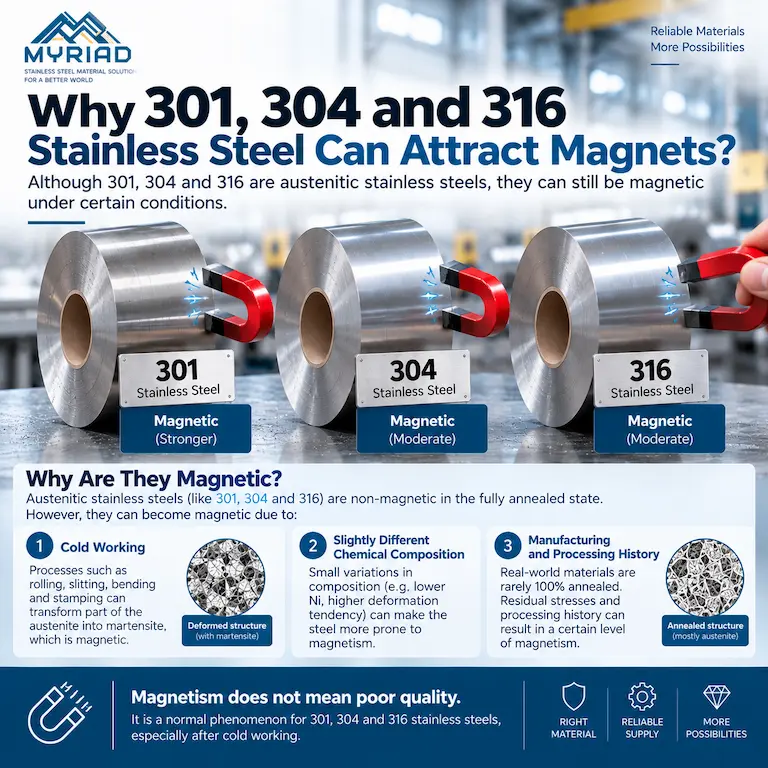
Austenitic stainless steel can develop magnetic response when cold working transforms some austenite into martensite. The result depends on composition and processing history. Wrought, annealed material and a heavily formed part should therefore not be assumed to have the same magnetic behaviour. ASSDA explains this transformation in its magnetic-effects technical FAQ.
Properly annealed 301 has low magnetic response. Cold working can transform some of its austenite into ferromagnetic martensite, increasing magnetic permeability. This makes processing condition especially relevant when evaluating cold-rolled 301 strip for springs or clips. Brown Metals describes both the transformation and the range of properties obtainable through chemistry and temper rolling in its 301 technical data sheet.
Half-hard and full-hard 301 are cold-worked conditions, so a magnetic response is not, by itself, evidence of incorrect material. However, temper describes mechanical requirements; it does not assign a universal permeability value. Do not convert a hardness or tensile-strength result into a magnetic acceptance result without an agreed, validated basis.
Compare samples in the condition relevant to the application. Annealed 316 and full-hard 301 are not a controlled comparison of grade alone. Record temper, processing history and measurement conditions before drawing conclusions about their magnetic response.
For 301 spring strip, evaluate the combination of required strength, forming behaviour and magnetic limits. For 304 or 316 alternatives, confirm those same requirements rather than selecting solely on a magnet test. The practical question is which grade and manufacturing route meet the finished-part specification—not which grade name sounds least magnetic.
It can be. Cold rolling, drawing and forming can produce magnetic martensite in 304. A measurable change after fabrication does not automatically mean the original material was incorrectly supplied. The amount of transformation is not determined by the grade name alone. Carpenter discusses the influence of cold work and composition in its magnetic properties guide.
When buying 304 stainless steel foil, separate the requested temper from the magnetic acceptance requirement. “304” identifies the alloy designation; it does not specify a maximum permeability for every thickness and manufacturing route.
Properly annealed wrought 316 normally has low magnetic response. It generally develops less magnetic response from cold work than 304, but “316 is never magnetic” is too absolute. ASSDA describes 316’s annealed and cold-worked behaviour in Grade 316: The First Step Up.
Treat 316 as a candidate to evaluate for a low-permeability application, not as automatic proof of compliance. Ask for the condition of the delivered product and assess the finished component against the specified limit. Substitution should also consider the application’s other material requirements.
Weld metal and austenitic castings can contain ferrite and consequently have higher magnetic permeability than wrought parent material. A response concentrated near a weld therefore deserves a different investigation from a response distributed across cold-worked strip. This distinction is covered by the British Stainless Steel Association.
A useful inspection record identifies the location: flat stock, formed corner, weld or adjacent component. Recording only “magnetic” loses information that could explain the observation.
Magnetic permeability describes how a material responds to an applied magnetic field. Relative permeability, written as µr, compares that response with the permeability of vacuum. For low-magnetic material, a value close to 1 is the relevant concept; “non-magnetic” does not mean a permeability of zero.
Carpenter reports DC relative permeability of about 1.003–1.005 at 200 oersteds, approximately 16 kA/m, for fully austenitic, well-annealed stainless steels. These are reference values under stated conditions, not a guaranteed range for every 301, 304 or 316 coil. See Carpenter’s magnetic properties discussion.
Three observations should remain separate:
Observation or property | What it addresses | How to use it in a specification |
Attraction to a magnet | A qualitative response in a particular setup | Use as an agreed screening check, not a numerical permeability result |
Relative permeability | Response to an applied magnetic field | State the limit, method and applicable measurement conditions |
Residual magnetic field | Field remaining after magnetising exposure | Specify separately if it affects the assembly’s function |
Demagnetising treatment can reduce residual magnetisation, but it does not remove the magnetic phase created by cold work. Solution annealing can change the microstructure, yet it also changes mechanical properties and may affect dimensions. It is not a routine remedy to apply without engineering review. ASSDA: Magnetic Effects of Stainless Steel.
For an enquiry, replace “must be completely non-magnetic” with a measurable requirement. If the engineering team has not established a limit, describe the sensitive equipment, the position of the component and the manufacturing sequence. That gives the responsible engineer a basis for selecting acceptance criteria instead of importing an arbitrary value from a general article.
Use different checks for different questions. Grade verification concerns alloy identity; permeability testing concerns magnetic response. A handheld magnet cannot provide both answers. Start by deciding whether the inspection is intended to identify mixed stock, qualify material for a sensitive application, or investigate a change after fabrication.
Check material documentation and lot traceability. Where additional verification is required, choose an appropriate chemical-analysis method. X-ray fluorescence can help identify alloy composition, but conventional XRF does not measure carbon and cannot by itself distinguish 304 from 304L or 316 from 316L. ASSDA: Testing for Grade Confirmation.
Keep the grade record and the magnetic test record linked to the same sample. Otherwise, two valid reports may still fail to demonstrate the properties of the material actually supplied.
ASTM A342/A342M-26 covers weakly magnetic materials with relative permeability not exceeding 6. Its methods are not interchangeable in every situation. Methods 1 and 5 allow selection of the applied field, which must be specified; Methods 3 and 4 use locally varying fields that cannot be specified in the same way. Sample shape and size also constrain applicability. See the ASTM public scope.
The practical implication is to agree the method with the laboratory before writing a numerical acceptance limit. For foil or narrow strip, ask whether the actual thickness, width and sample geometry are suitable. Do not assume a method demonstrated on a larger specimen is validated for a very thin strip.
A useful report should identify the lot, sample condition, method, applicable instrument setup, tested locations and result. Include field strength where the chosen method defines or controls it. These are recommended procurement details; the full applicable standard and agreed inspection plan govern the actual procedure.
Coilover Springs: Characteristics, Materials, and Applications
Specify the required behaviour at the stage when it matters. Incoming-material approval alone may not answer a requirement for a formed or welded part. Give the supplier the material dimensions and processing route, then agree what evidence is needed before a sample or production lot can be accepted.
The following examples are decision scenarios, not reported customer cases or test results.
Scenario 1: A spring made from half-hard 301 strip attracts a magnet. Check the supplied temper and compare retained incoming strip with the formed spring. Magnetic attraction may already be present before forming. If the assembly has a magnetic limit, evaluate both stages and retain the mechanical requirements; annealing simply to reduce magnetic response may remove the cold-worked strength the spring needs.
Scenario 2: A 316 strip component sits near a sensitive sensor. Give the supplier the engineering limit and proposed test method, together with the bending and joining sequence. Arrange prototype evaluation at the relevant stage. Do not release the drawing with only “316, non-magnetic” as the magnetic requirement.
Scenario 3: A component must respond strongly to an electromagnetic field. A low-permeability austenitic grade may be the wrong starting point. Carpenter describes soft magnetic ferritic stainless steels for electromechanical devices, where permeability, coercivity and residual induction matter. Evaluate that material category with the designer rather than choosing solely by magnet attraction. Carpenter: Ferritic Steels for Electromechanical Devices.
For Myriad foil and precision-strip enquiries, send these details for feasibility review. Any specified magnetic limit, test arrangement or finished-part requirement needs explicit confirmation for the proposed supply. General grade information is not a magnetic-performance guarantee.
For enquiries about work-hardened 301 material, refer to the 301 discussion on this page and define the supplied condition and acceptance evidence.
No. Ferritic, martensitic and duplex families are magnetic, while austenitic material generally has low response in a suitable annealed condition. Processing can change the result, so identify both grade and condition.
A stable austenitic structure has low relative permeability and is commonly described as non-magnetic. That description does not mean zero response under every measurement condition.
It can show appreciable magnetic attraction because cold working can form martensite. The full-hard designation alone does not guarantee a particular permeability or magnet-pull result. Specify and test magnetic performance separately if it affects the application.
No, not reliably. All three grades can have low attraction in an annealed condition, and processing affects the response. Use traceable material records and suitable chemical identification when grade confirmation is needed.
Some austenitic grades can retain low magnetic response, but the result must be evaluated for the actual processing route. A general “non-magnetic steel” label is not a substitute for testing at the agreed acceptance stage.
No. The grade name alone does not establish compliance with a particular limit. Although 316 generally responds less strongly to cold working than 304, acceptance should be based on the specified condition and measurement.
Always Provides You with the BEST Austenitic Stainless Steel Products